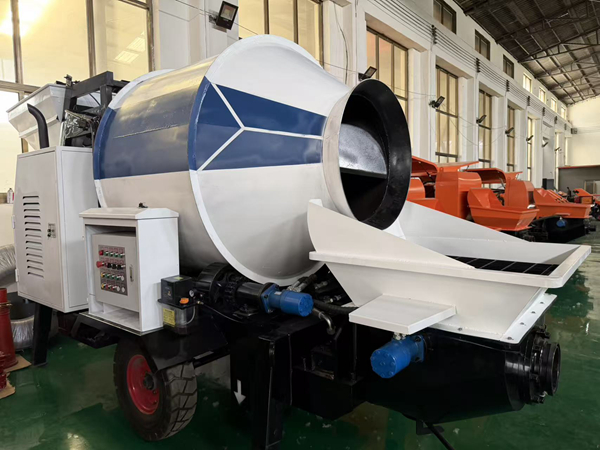
The Model 50 integrated mixer pump combines a JZC/JS500 mixer and an HBT50 pumping system on a single trailer chassis, integrating feeding, mixing and pumping in one unit. No separate mixer is needed, making it suitable for sites without a ready-mixed concrete station and for field or mountain projects: concrete is mixed on site and pumped directly. Available in electric and diesel versions (the whole unit driven by a diesel engine).
Core Technical Parameters (Common Industry Version)
·Theoretical pumping output: 50 m³/h, actual output on site is 30–36 m³/h
·Mixing unit: 500 mixer (0.5 m³ output per batch), drum type / compulsory twin-shaft type optional
·Power options:
·Electric version: main pumping 55 kW + mixing + feeding motors, 380 V industrial power
·Diesel integrated unit: 4110 turbocharged diesel engine, one engine for the whole machine, no external power supply needed
·Maximum pumping pressure: 10–12 MPa, high/low pressure switching
·Conveying distance: vertical 80–100 m, horizontal 200–280 m (compared with a stand-alone Model 50 ground pump, the built-in mixer raises the centre of gravity, so the conveying distance is slightly shorter than that of a pure Model 50 trailer pump)
·Conveyable aggregate: crushed stone ≤40 mm, pebble ≤50 mm; site-mixed ordinary concrete, fine aggregate and mortar are all acceptable
·Delivery pipeline: mainly DN125
·Distribution valve: S valve, twin-cylinder hydraulic piston pumping; mixed material flows automatically into the pump hopper
·Control: wired + wireless remote control, one-key switching between forward and reverse pumping, reverse suction when blocked
·Overall weight: 4800–5600 kg, with a trailer chassis and towing hook, towed by truck for relocation
·Cooling: water cooling, suitable for long continuous mixing + pumping operation
Working Principle
Sand, gravel, cement and water enter the machine's 500 mixer drum through the feeding mechanism, and after being mixed evenly are automatically discharged into the pump hopper. The hydraulic pumping system, through the S-valve piston, conveys the mixed concrete directly through the pipeline to the pouring point. A single machine completes both batching/mixing and concrete pumping, without the need for two machines working together.
Applicable Project Scenarios
1. House building in remote townships and mountain areas without a ready-mixed concrete station: on-site mixed concrete for pouring multi-storey buildings, ground beams, columns and floor slabs
2. Water conservancy projects: river embankment slope protection, channel lining, small dams and reservoirs
3. Rural road hardening, photovoltaic foundations, small culverts, retaining walls and foundation pit blinding
4. Plant floors and large-area site hardening; can also be used for fine aggregate floor heating backfill
Selection advice: choose the electric mixer trailer pump if power is available; for field sites without a power grid, choose the diesel integrated mixer pump.
Main Advantages
1. One machine, two uses: with its own mixer, there is no need to buy a separate mixer or use a loader to transfer material, reducing equipment investment and labor and taking up less site space
2. Concrete is mixed on site, a huge advantage at remote sites without ready-mixed concrete; no need to haul ready-mixed concrete over long distances, saving freight
3. Mixed material goes directly into the pump hopper, so the concrete does not segregate and continuity is good
4. Wear-resistant S valve with reverse pumping function makes blockage easy to clear; high/low pressure mode switching balances distance and output
5. Integrated trailer design allows the whole machine to be relocated, saving moving time; ideal for contractors with many projects and frequent site changes
[Key Comparison] Standard Model 50 Delivery Pump VS Model 50 Integrated Mixer Pump
|
Item |
Model 50 Standard Concrete Pump (HBT50) |
Model 50 Integrated Mixer Pump (JBT50 Mixer Trailer Pump) |
|
Mixing Function |
None; an external mixer / ready-mixed concrete tanker is needed to feed it |
Built-in 500 mixer for on-site mixing |
|
Theoretical pumping output |
50m³/h |
50m³/h |
|
Maximum vertical conveying |
130–150m |
80–100m |
|
Overall Weight |
3.8–4.5 t |
4.8–5.6 t |
|
Suitable Scenarios |
With ready-mixed concrete and a separate mixer feeding, for high-rise long-distance pumping |
Remote sites without a ready-mixed concrete station, concrete mixed on site |
|
Equipment Investment |
Pump + separate mixer, two sets of equipment |
One complete machine, one-time purchase |


